Process Chiller Maintenance Checklist
A maintenance checklist for process chillers — glycol concentration and inhibitor condition, reservoir and filtration, holding tight temperature tolerance under continuous duty, redundancy changeover testing, and planning maintenance around a plant with no shutdown window.
Also available as editable Excel and Word — with asset, sign-off and findings columns.
What is a process chiller maintenance checklist?
A process chiller maintenance checklist is a structured list of the 16 preventive maintenance tasks — covering visual, functional, cleaning, safety and record-keeping checks — that keep a process chiller running safely and reliably. It groups routine checks by frequency, from daily inspections to annual servicing, so FM teams and building engineers can plan and evidence preventive maintenance.
Core process chiller checks
- Check reservoir or buffer tank level, top-up arrangements and internal cleanliness, and inspect for sediment and biological growth
- Measure glycol concentration with a refractometer and confirm the freeze point and burst protection against the process requirement
- Clean or replace process circuit filtration
- Test redundancy
- Confirm the correct glycol type is in use and recorded
What is a process chiller?
A process chiller cools a manufacturing process rather than a building. It serves injection moulding, laser and machine tool cooling, pharmaceutical and biotech production, food and beverage processing, or data centre and laboratory equipment. The refrigeration circuit is broadly the same as a comfort cooling chiller; almost everything about how it is operated and maintained is different.
Three things drive that difference. The first is duty: a process chiller typically runs continuously, without the seasonal shutdown that gives a comfort cooling machine a natural maintenance window. The second is tolerance: comfort cooling is judged on whether the space feels right, whereas a process chiller often has to hold a setpoint within a fraction of a degree, because the product or the equipment depends on it. The third is consequence: when a comfort chiller fails the building gets warm, but when a process chiller fails a production line stops, a batch is scrapped, or expensive equipment is damaged.
That last point reframes the maintenance economics entirely. On a comfort cooling machine, deferring a service is a manageable risk. On a process chiller, the cost of an hour of unplanned downtime routinely exceeds the annual maintenance budget, which is what justifies condition monitoring, held spares and genuine redundancy on plant that would look over-maintained in a commercial building.
This checklist is one of 34 in our HVAC maintenance checklists, covering air handling units, fan coils, chillers, VRF, ductwork and extract systems — filters, coils, refrigerant and damper checks.
Typical Process Chiller maintenance checklist
A practical starting point for planned preventive maintenance. Always refer to the manufacturer's O&M manual and site-specific requirements.
Visual Checks
- Check reservoir or buffer tank level, top-up arrangements and internal cleanliness, and inspect for sediment and biological growth
Functional Checks
- Measure glycol concentration with a refractometer and confirm the freeze point and burst protection against the process requirement
- Test glycol condition — check pH and inhibitor reserve, and look for the colour change and acidity that indicate degradation
- Verify delivered fluid temperature stability against the process tolerance over a full load cycle, not just at a single point
- Check setpoint, control deadband and any cascade or PID tuning against the process requirement and the commissioning record
- Review load matching and buffer volume — check the cycle pattern against the process load profile for short cycling on light load
- Take a compressor oil sample for analysis including acidity, and trend the result rather than reading it in isolation
- Carry out vibration analysis on compressors and pumps where continuous duty justifies condition monitoring
- Record suction and discharge pressures and verify superheat and subcooling against the manufacturer's target range
Cleaning & Housekeeping
- Clean or replace process circuit filtration — strainers, bag or cartridge filters and any side-stream filtration
Safety Checks
- Test redundancy — run the duty/standby or N+1 changeover and confirm the standby machine achieves setpoint within the required time
- Confirm automatic changeover on fault actually operates, rather than assuming it will because it is configured
- Test safety controls and confirm process-critical alarms route to somewhere staffed at the times the plant runs
Record Keeping
- Confirm the correct glycol type is in use and recorded — inhibited industrial glycol, never automotive antifreeze, and propylene where food or pharmaceutical contact is possible
- Record compressor run hours and starts per hour, and trend against the previous visit
- Update the F-Gas logbook and confirm the leak check interval is being met given continuous operation
Download the free Process Chiller maintenance checklist PDF
Get all 16 tasks as a printable PDF — free, no signup needed. Keep a copy in the plant room, attach it to work orders, or share it with your maintenance contractor.
The PDF is free and needs nothing. The Excel and Word versions add asset details, sign-off and findings columns so you can record the work as you do it — we ask for an email address for those.
Typical maintenance frequency
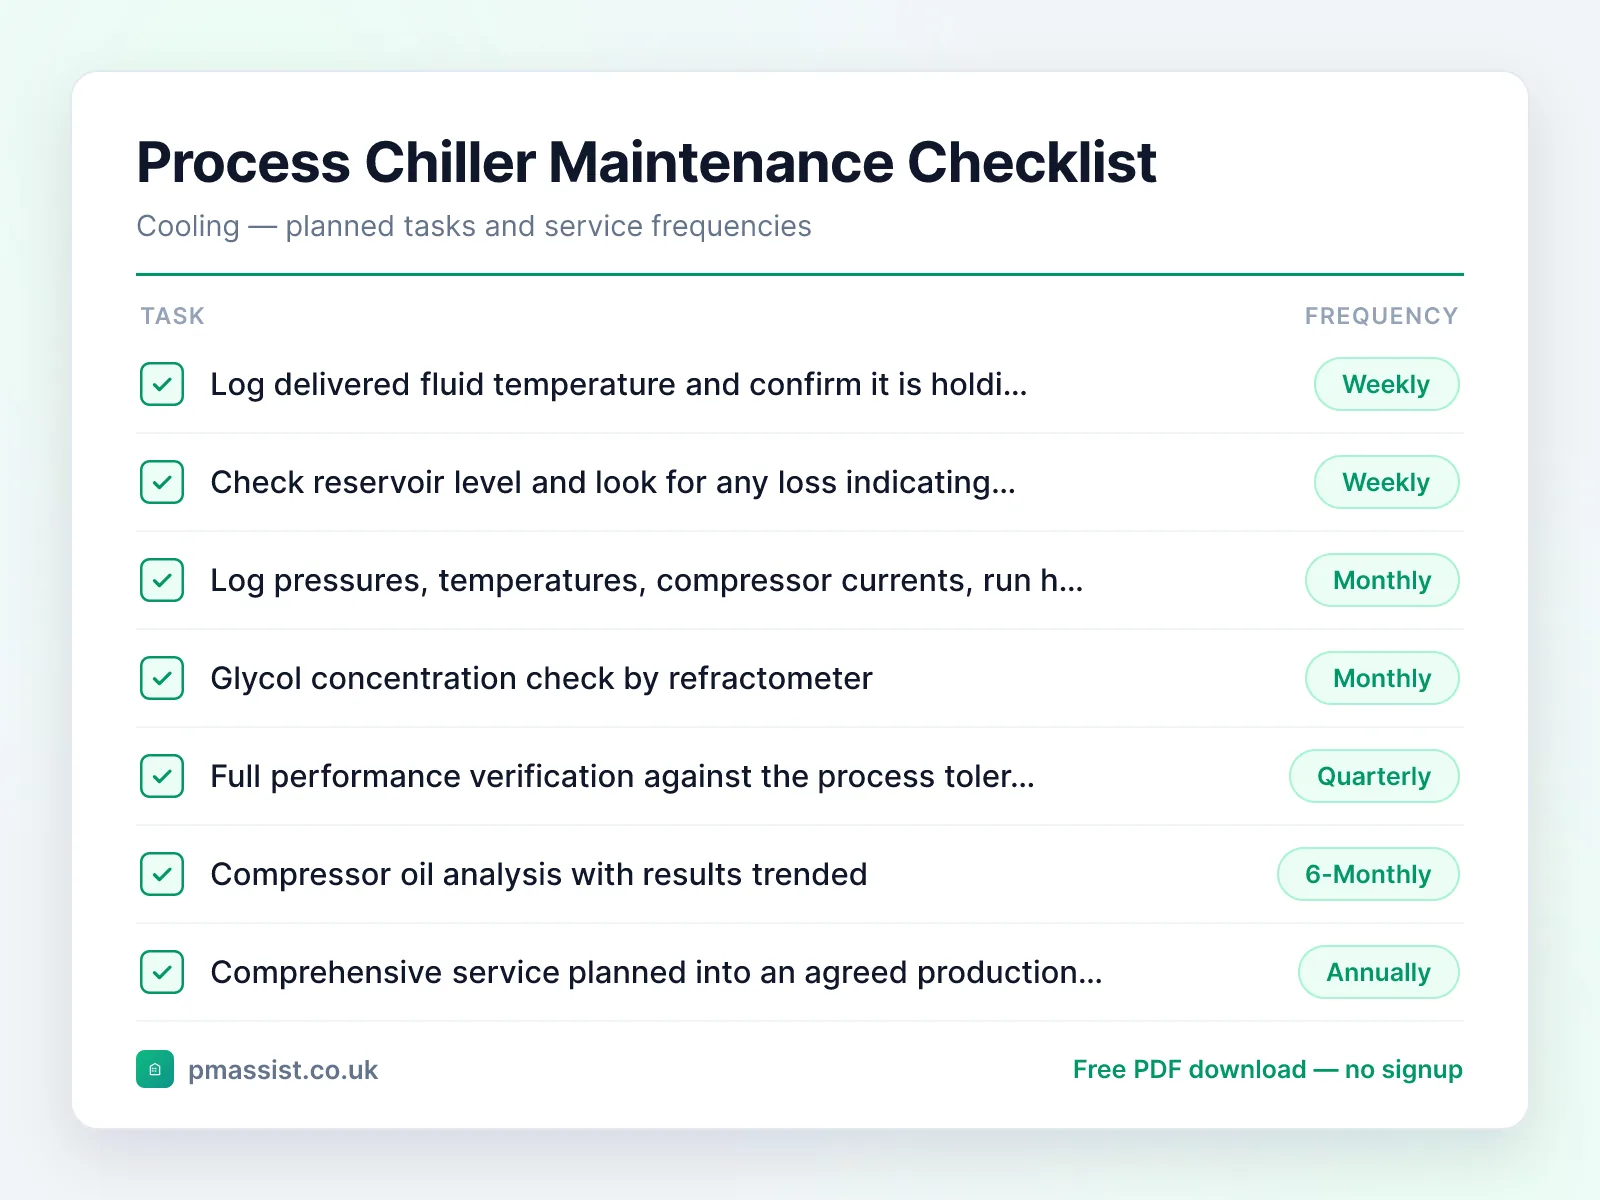
Suggested intervals for process chiller maintenance. Actual frequencies should follow manufacturer guidance and site-specific risk assessments.
Weekly
- •Log delivered fluid temperature and confirm it is holding within the process tolerance
- •Check reservoir level and look for any loss indicating a leak in the process circuit
- •Review alarm history since the last check
Monthly
- •Log pressures, temperatures, compressor currents, run hours and starts
- •Glycol concentration check by refractometer
- •Filter differential pressure check and clean or replace as required
Quarterly
- •Full performance verification against the process tolerance across the load range
- •Duty/standby changeover test with the standby machine proven to setpoint
- •Safety control and critical alarm routing test
- •Glycol inhibitor and pH testing
Every 6 Months
- •Compressor oil analysis with results trended
- •Vibration analysis on compressors and process pumps
- •Reservoir inspection and clean where the process permits access
- •F-Gas leak check where the charge places the unit on a six-monthly interval
Annually
- •Comprehensive service planned into an agreed production shutdown window
- •Compressor oil and filter change
- •Condenser clean appropriate to the machine's heat rejection type
- •Electrical thermography of panel and motor terminations
- •Review of held spares against lead times for the critical components
- •F-Gas leak check and logbook update at the interval set by the CO₂e charge
Common faults and issues
Issues to be aware of when maintaining process chiller equipment.
Safety and compliance notes
Key safety considerations for process chiller maintenance. This is general guidance only — always follow OEM instructions, statutory requirements, and your organisation's safe systems of work.
Reference standards and frameworks
- United Kingdom
- SFG20, CIBSE Guide M, and the UK F-Gas Regulations for refrigerant plant
- North America
- EPA Section 608 refrigerant handling rules, which apply whatever the equipment serves
- Middle East
- Dubai Municipality's Green Building Regulations require commissioning to CIBSE Commissioning Code R (refrigeration systems)
ASHRAE/ACCA Standard 180 is not cited here. Its scope clause (§2.2(b)) excludes equipment that primarily serves an industrial, manufacturing or commercial process, so it does not apply to a process chiller even though it is the usual reference for comfort-cooling plant.
Frameworks commonly referenced when planning process chiller maintenance programmes. Always confirm the requirements that apply to your site and jurisdiction.
Managing Process Chiller documentation with PM Assist
PM Assist helps FM and building operations teams search their O&M manuals and building drawings in seconds. Upload your process chiller documentation and ask questions like “What is the rated cooling capacity?” or “When was the last F-Gas leak check?” — and get source-cited answers instantly.
The checklist tells you what to check. The manual tells you the numbers.
Ask a process chiller manual a question and get the answer back with the page it came from. No signup, and you can drop in your own PDF instead of the sample.
“What is the rated cooling capacity?”Runs against a sample chiller manual so you can see the shape of the answer — then try it on one of yours.
Take this checklist with you
Download the branded PDF, generate a custom version for your asset, or run AI search across all your building documentation.
Related maintenance checklists
Chiller maintenance checklist
Cooling · 18 tasks
Air-Cooled Chiller maintenance checklist
Cooling · 16 tasks
Water-Cooled Chiller maintenance checklist
Cooling · 17 tasks
CRAC Unit (Computer Room Air Conditioning) maintenance checklist
Cooling · 10 tasks
Pump maintenance checklist
Pumps & Pressurisation · 12 tasks
Water Treatment Unit maintenance checklist
Water Systems · 10 tasks
Further reading on process chiller maintenance
Compliance topics for process chiller maintenance
Refrigerants used in process chiller
GWP, the charge in kg at which leak checks start, and the Great Britain and Northern Ireland figures side by side.
Compliance & CAFM
Run process chiller maintenance in PM Assist
This checklist is also a planned maintenance programme in PM Assist, included in every paid plan alongside the compliance register and mobile inspections.
- Add a process chiller to a building's asset register and this maintenance programme is created for you, with each task on its frequency in the planner.
- F-Gas Leak Check is tracked on the compliance register, with the date last done, the date next due and the certificate.
- Contractors can be given a login to see their jobs and upload certificates.
Frequently asked questions
How is process chiller maintenance different from building chiller maintenance?
What glycol concentration should a process chiller run at?
How often should glycol be tested and changed?
How do you maintain a process chiller with no shutdown window?
Why does my process chiller short cycle on light load?
Does a process chiller need N+1 redundancy?
What condition monitoring is worth doing on a process chiller?
What temperature tolerance should a process chiller hold?
Manage your building documentation with AI
PM Assist gives FM teams instant access to O&M manuals, drawings, and maintenance knowledge — all searchable with AI.
- Upload and organise building documentation
- AI-powered search across all your manuals
- Source-cited answers for maintenance queries
- Team collaboration and access control
- No credit card required to start